How to Design for Progressive Die Stamping: A Practical DFM Guide
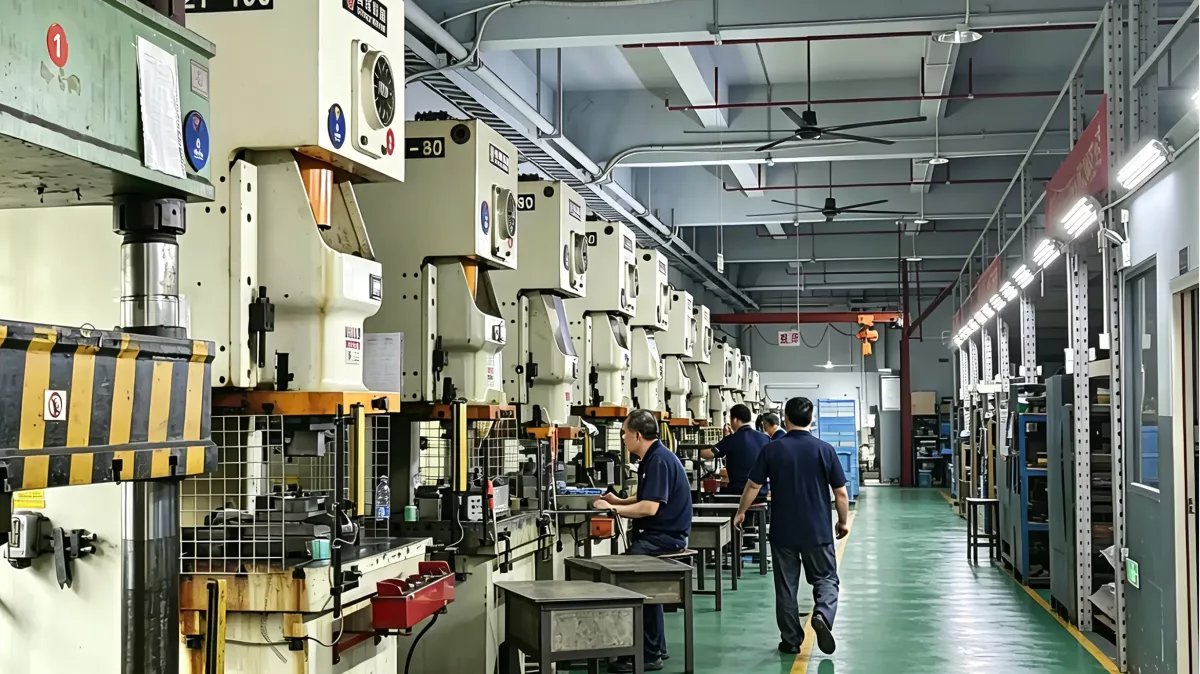
Progressive die stamping produces parts in a continuous strip, with each station performing one or more operations. The design of the strip layout often determines material utilization, tool life and part consistency.
This guide covers the practical decisions that affect a progressive die project, from strip layout to datum strategy.
1. Start with the strip layout
The strip layout shows the sequence of cuts, bends and forms, the carrier, the pilot holes and the scrap. A good layout minimizes stations, keeps the strip stable and uses material efficiently.
2. Choose the carrier
The carrier holds the part as it moves through the die. Common options are a center carrier, a single-side carrier and a double-side carrier. The choice depends on part shape, stability and the amount of forming.
3. Use pilot holes
Pilot holes locate the strip precisely at each station. They should be placed in a stable area and used consistently as the datum for inspection.
4. Plan the forming sequence
Bends and draws should be sequenced so that material is not trapped or over-stretched. Forming in the wrong order can cause tearing, distortion or difficulty stripping the part.
5. Design for material utilization
Nesting and strip width affect material cost, which is often the largest part of the unit price. A small improvement in utilization can be significant at volume.
6. Define the datum and inspection plan
Use a clear datum scheme that matches the function of the part. If the part is inspected on a CMM, the datum should be accessible and stable. Avoid using a feature that is formed late in the strip as the primary datum.
7. Consider tool maintenance
Sharp corners, narrow sections and hard materials increase wear. Design with replaceable inserts where possible, and plan for sharpening and spare parts.
Progressive die DFM checklist
- Strip layout and material utilization reviewed.
- Carrier type selected and strip stability confirmed.
- Pilot holes defined and used as datum.
- Forming sequence checked for tearing and stripping.
- Bend radii and hole spacing within guidelines.
- Tool wear points identified; replaceable inserts considered.
- Inspection plan and critical dimensions agreed.
FAQ
How many stations does a progressive die need?
It depends on the number of cuts, bends and forms. Simple brackets may need 5-8 stations; complex parts can need 15 or more.
Can a progressive die make drawn parts?
Yes, progressive dies can include drawing stations, but the draw depth and material must be planned carefully. Deep draws may be better on a transfer or single-hit process.
What is a reasonable tool life?
It depends on material, coating, die steel and maintenance. Ask the toolmaker for the expected sharpening interval and the number of strokes between services.
Related: stamping capabilities and send a drawing for DFM.
 WhatsApp